Note: This article contains affiliate links. If you click on these links and make a purchase, we may earn a small commission at no extra cost to you. This helps support our research and content. Read our full affiliate disclosure here.
If you plan to print strong, wear-resistant parts, choosing the right 3D printer for nylon matters more than with consumer filaments. Nylon demands higher extrusion temperatures, tight thermal control, and often a dry, controlled build environment to avoid warping and moisture-related print failures. This guide covers seven shortlisted printers that are well suited to working with nylon and similar engineering materials. We explain the practical tradeoffs—hotend and nozzle choices, enclosure and bed systems, filament handling, and adhesion strategies—so you can pick a machine that meets your part-strength, dimensional, and workflow needs. Read on for the top picks and the criteria used to evaluate them.
Top Picks at a Glance
| Best Overall The best all-around choice for most situations | HEPHi3D TINA2S 3D Printer |  |
| Best Quality Built to a higher standard if you want something more solid | Bambu Lab A1 Mini Combo |  |
| Best Value The sweet spot between price and what you get | Anycubic Kobra X |  |
| Best Budget The cheapest option that still gets the job done reliably | Creality Ender 3 V3 SE |  |
| Top Rated A top-rated pick with lots of positive feedback | ELEGOO Neptune 3 Pro |  |
| Most Popular A crowd favorite that many people choose with confidence | FLASHFORGE Adventurer 5M |  |
| Best Seller A high-volume bestseller chosen again and again | Creality K2 Combo 3D Printer |  |
HEPHi3D TINA2S 3D Printer

| Compatible filaments | PLA, PLA Pro, TPU |
|---|---|
| Connectivity | WiFi app, TF card, USB |
| Features | Auto bed leveling, filament sensor, power-loss resume |
| Noise level | 40–50 dB |
The HEPHi3D TINA2S is a small, out-of-the-box FDM printer aimed at beginners and family/STEM use. It arrives fully assembled and claims a five-minute setup with auto bed leveling, filament sensor, and power-loss resume to reduce failed prints. Control options include a WiFi-enabled mobile app with a large cloud model library for one-tap wireless printing plus support for common slicers via TF card or USB. The printer emphasizes quiet operation with a custom motherboard and a semi-enclosed footprint that saves desk space and lowers accidental contact. Practical benefits include easy model access for learners, a magnetic flexible build plate for simple part removal, and compatibility with PLA, PLA Pro, and TPU for most casual projects. Important limitations for the article goal: the spec sheet and marketing do not list a heated chamber, high nozzle temperatures, or explicit Nylon compatibility, so this unit is best for PLA-family materials rather than engineering nylons that need higher extrusion and enclosure control. Advanced users seeking nylon-capable prints will likely need a machine with higher temperature range and a heated enclosure.
Best for: Buyers who want a compact, easy-to-use first printer for family projects, classroom STEM learning, or hobbyist PLA/T TPU printing with minimal setup and mobile control.
Less Ideal for: Users who need to print engineering-grade materials like Nylon, or who require a heated enclosure and high-temperature hotend for demanding functional parts.
- Fully assembled and beginner-friendly with auto bed leveling for quick startup
- WiFi app and cloud library with one-tap printing for easy model access
- Filament sensor and power-loss resume reduce failed prints and material waste
- Quiet operation and compact semi-enclosed design suitable for home and classroom use
- No specification of high-temperature nozzle or enclosed heated chamber needed for reliable Nylon printing
Verdict: Choose the TINA2S if you want a compact, fully assembled beginner printer with easy app-driven printing and reliable PLA-family results, but not for Nylon parts.
Bambu Lab A1 Mini Combo

| Build Volume | 180×180×180 mm³ |
|---|---|
| Max Speed | 500 mm/s |
| Max Acceleration | 10 m/s² |
| Supported Filaments | PLA, PETG, TPU, PVA |
The Bambu Lab A1 Mini Combo pairs a compact, high-speed core printer with the AMS lite accessory to enable multi-color and multi-part prints without complex slicing workarounds. It is aimed at users who want fast, accurate results out of the box: the printer ships pre-assembled, uses full-auto calibration (Z-offset and bed leveling), and offers active flow rate compensation to stabilize extrusion for smoother surfaces. The 1-Clip quick-swap nozzle and quiet motor noise cancellation make maintenance and long prints easier, while the touchscreen simplifies job setup so a first print can be ready in roughly 20 minutes. Practical limits include a relatively small 180 × 180 × 180 mm build volume and an open-frame design that is less suitable for high-temperature filaments unless external enclosure measures are used. Still, for PLA, PETG and flexible filaments and for users focused on speed and reliable multi-color output, the A1 Mini Combo delivers a polished, production-minded experience in a small footprint.
Best for: Buyers who prioritize speed, reliable multi-color capability, and quick setup for prototyping and small production runs, especially when working mainly with PLA, PETG, or flexible filaments.
Less Ideal for: Users who need large-format printing or who plan to print high-temperature engineering nylons regularly without adding an enclosure or upgrades.
- Fast printing with high acceleration for shorter print times
- Full-auto calibration reduces setup time and leveling hassle
- AMS lite enables reliable multi-color printing without manual filament swaps
- Active flow rate compensation improves extrusion consistency
- Pre-assembled design and touchscreen make first prints quick and easy
- Small build volume limits larger functional nylon parts
- Open-frame design and filament support list indicate limited out-of-the-box high-temperature material capability
Verdict: Choose the A1 Mini Combo if you want a compact, high-speed printer that delivers fast, multi-color prints with minimal setup for prototyping and small runs.
Anycubic Kobra X

| Build volume | 260×260×260 mm³ |
|---|---|
| Max hotend temp | 300C |
| Multicolor support | Native 4-color, expandable to 19 |
| Noise level | ≤48 dB |
| Camera | 720p AI monitoring |
The Anycubic Kobra X is a user-oriented FDM printer that focuses on speed and multicolor capability while keeping setup simple. It uses LeviQ 3.0 automatic bed leveling with 49-point probing and vibration compensation to deliver consistent first layers without manual fiddling, and built-in sensors for filament run-out and power-loss recovery make long prints more reliable. ACE GEN2 multicolor handling and support for up to 19 colors (with additional hubs) suit decorative or prototype parts, while the hardened steel nozzle and 300C hotend let you print a variety of filaments including PLA, PETG, TPU, PVA and ASA. The integrated 720p camera and AI detection help catch print failures early. Where it differs from machines optimized for engineering plastics is its emphasis on speed—rated up to 600 mm/s—which accelerates production but may require tuning for demanding materials. For Nylon specifically, the Kobra X can reach the temperatures and filament handling needed, but users should plan on drying filament (the ACE 2 Pro offers active drying) and tuning cooling and print speed for strong, low-warp Nylon parts.
Best for: A practical buyer who wants a fast, reliable desktop printer that minimizes setup time and handles a broad range of filaments with room to add multicolor capability as projects demand.
Less Ideal for: Users seeking a dedicated industrial Nylon workstation for large structural parts or who need an enclosed, actively heated chamber for minimal warping on large Nylon prints should consider a fully enclosed, high-temperature specialty machine instead.
- Automatic 49-point LeviQ leveling reduces setup and first-layer failures
- Hardened steel nozzle and 300C capable hotend support higher-temp filaments
- Built-in filament run-out and power-loss recovery improve print reliability
- ACE GEN2 multicolor system and expandability up to 19 colors for complex color prints
- 720p camera with AI detection for remote monitoring and failure prevention
- High advertised speeds require tuning and may need slower settings for Nylon to avoid layer adhesion issues
- Multicolor expansion requires additional ACE 2 Pro hubs and accessories to reach full color capability
Verdict: Buy the Kobra X if you want a fast, beginner-friendly printer that supports higher-temperature filaments and easy multicolor upgrades while reducing setup time.
Creality Ender 3 V3 SE
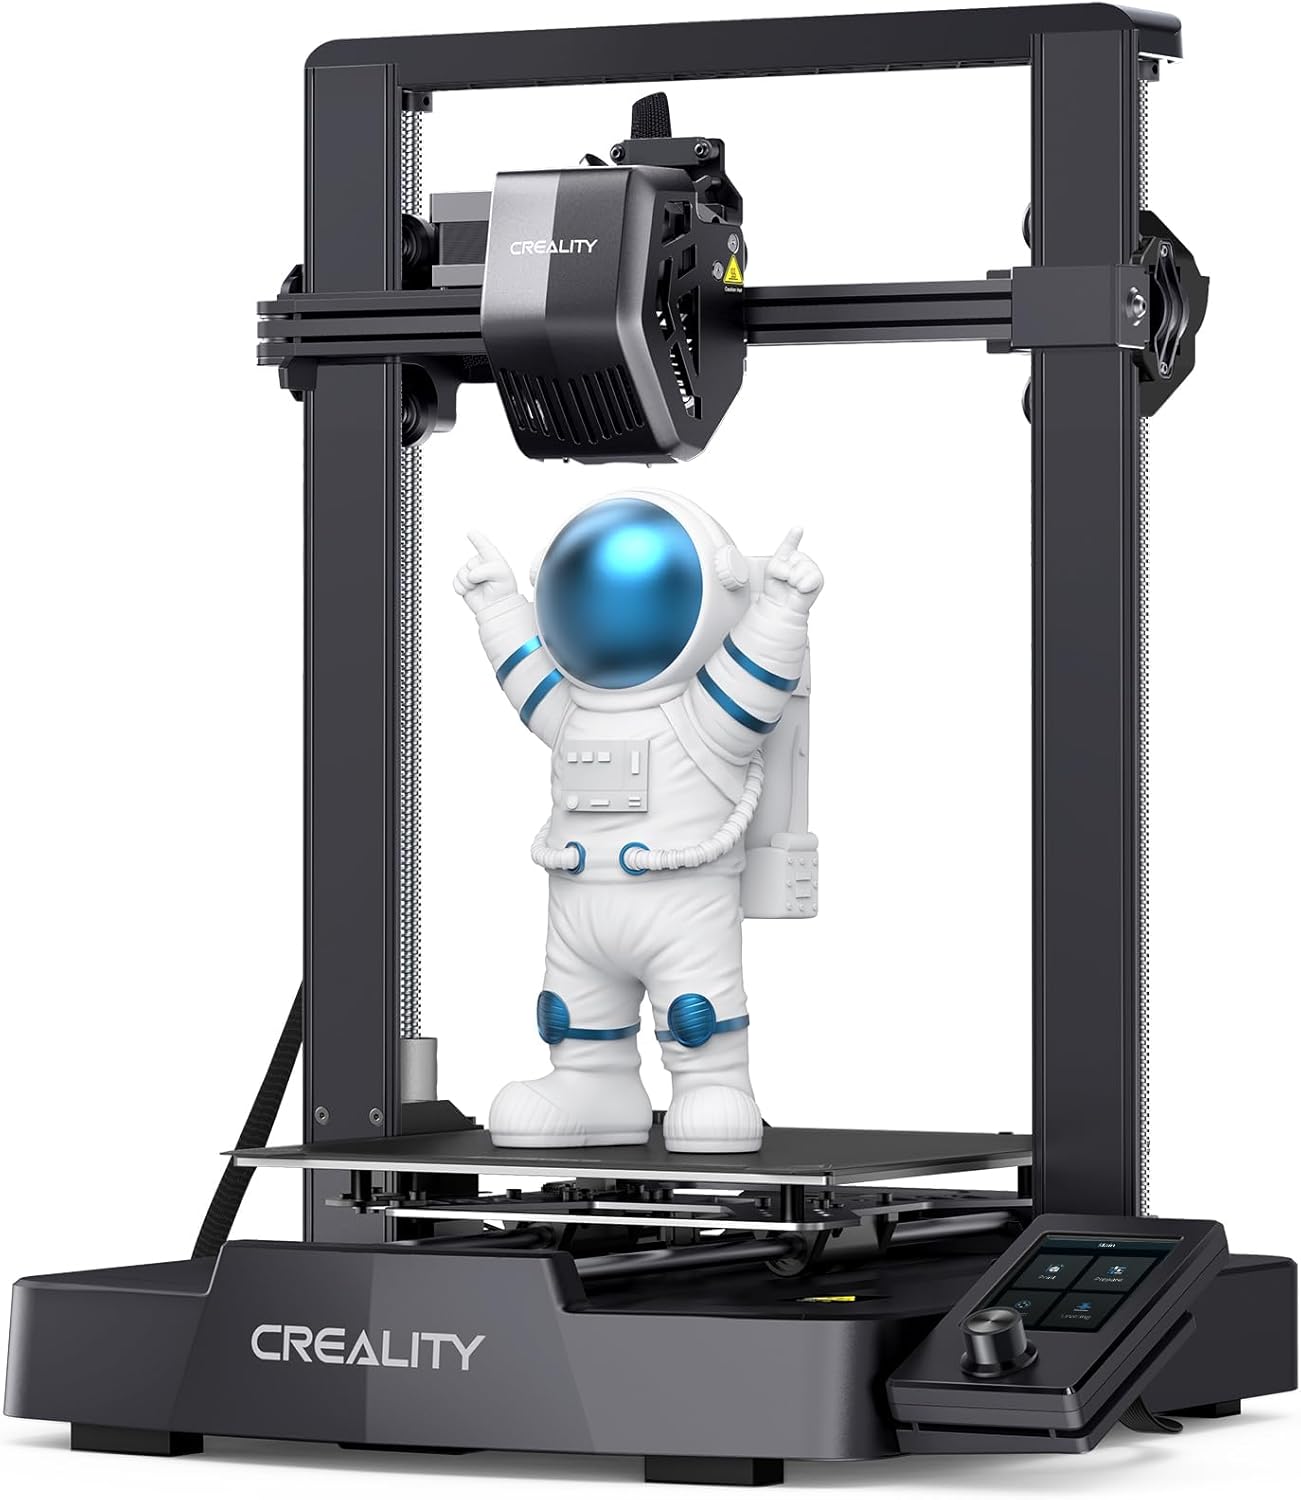
| Max printing speed | 250 mm/s |
|---|---|
| Printing method | FDM (SD card) |
| Extruder | Full-metal Sprite dual-gear direct extruder |
| Auto-leveling | CR Touch + strain sensor |
The Ender 3 V3 SE is a budget-minded desktop FDM printer that aims to speed up hobby and small-project printing without demanding a long setup. It ships partly preassembled and claims a three-step build that can get you from box to first print in about 20 minutes, and the updated UI and auto filament load make routine use easier. The full-metal Sprite dual-gear direct extruder provides stronger, more consistent filament feeding that helps with flexible and abrasive filaments, and the CR Touch auto-leveling plus a strain sensor handle bed leveling and Z-offset automatically. Dual Z-leadscrews and reinforced Y-axis linear shafts improve Z-axis stability for taller parts. Keep in mind the machine is positioned as an affordable desktop unit: while Creality advertises a 250 mm/s top speed, practical print quality for technical filaments like nylon will require slower speeds, good part cooling management, and an enclosure or dry filament storage to avoid moisture problems. For nylon users this printer gives capable hardware at a low entry price but you will likely need some filament drying and tuning for best results.
Best for: Someone buying an affordable, ready-to-run desktop printer who prioritizes reliable filament feeding, quick setup, and plan to experiment with engineering materials like nylon with some additional drying and tuning.
Less Ideal for: If you need out-of-the-box, consistently dry printing for hygroscopic materials in a production setting or want a factory-enclosed heated chamber, choose a printer with a built-in enclosure and active filament drying instead.
- Preassembled design that can be ready to print in about 20 minutes
- Full-metal Sprite dual-gear direct extruder for more reliable feeding of flexible and abrasive filaments
- CR Touch auto-leveling and strain sensor simplify bed leveling and Z-offset
- Dual Z-axis lead screws and robust Y-axis linear shafts for improved print stability
- Auto filament loading and upgraded UI reduce routine fiddling during filament swaps
- No enclosed build chamber, so nylon prints require external drying and an enclosure for reliable results
- Advertised top speed is high but maintaining print quality with technical filaments needs slower tuned settings
Verdict: If you want a low-cost desktop printer with a strong direct extruder and auto-leveling that can handle nylon with proper drying and tuning, the Ender 3 V3 SE is a practical entry choice.
ELEGOO Neptune 3 Pro

| Build volume | 225×225×280 mm |
|---|---|
| Noise level | ~47 dB |
| Filament diameter | 1.75 mm |
| Extruder type | Dual-gear direct drive |
The ELEGOO Neptune 3 Pro is a ready-to-assemble FDM desktop printer built for reliable, routine printing. It uses a dual-gear direct drive extruder with a 3:1 gear ratio and stainless steel components to deliver consistent filament feeding and reduced clogs, which is helpful when switching between flexible and stiffer materials. The printer includes 36-point auto bed leveling, a PEI magnetic build plate for easy part removal, filament runout detection, and power-loss resume so long prints are less likely to fail. Thermal upgrades—a titanium throat tube, brass nozzle, widened aluminum heat sink, and a front cooling fan—improve heat management for longer jobs. Dual lead screws and dual Z motors stabilize layer shifts for finer vertical accuracy. Noise is modest at about 47 dB during operation, and pre-assembled main parts plus a toolkit make setup straightforward. Limitations include the modest 225×225×280 mm build volume for larger nylon parts and the printer is not enclosed, which can make printing high-temp or hygroscopic nylons more challenging without an external enclosure and dry filament handling.
Best for: Buyers who prioritize dependable everyday printing and fewer failed prints will appreciate the Neptune 3 Pro’s focus on consistent filament feeding, auto leveling, and recovery features for routine workshop and hobby use.
Less Ideal for: Users who need to print large nylon parts or regularly print high-temperature, moisture-sensitive nylons without adding an enclosure or hotend upgrades should consider a different platform.
- Direct-drive dual-gear extruder for consistent filament feeding and fewer clogs
- 36-point auto bed leveling and PEI magnetic plate for reliable first layers and easy part removal
- Filament runout sensor and power-loss resume protect long prints from common interruptions
- Thermal and mechanical upgrades (titanium throat, improved heat sink, dual Z lead screws) enhance print stability and clog resistance
- Quiet stepper motors produce relatively low operational noise (~47 dB)
- Open-frame design and limited build volume can complicate printing high-temperature nylons without an enclosure
- No explicit high-temperature hotend spec provided, so very high-temp nylons may require aftermarket upgrades
Verdict: Choose the Neptune 3 Pro if you want a compact, reliability-focused desktop FDM printer with a robust direct-drive extruder and safety features that reduce failed prints.
FLASHFORGE Adventurer 5M
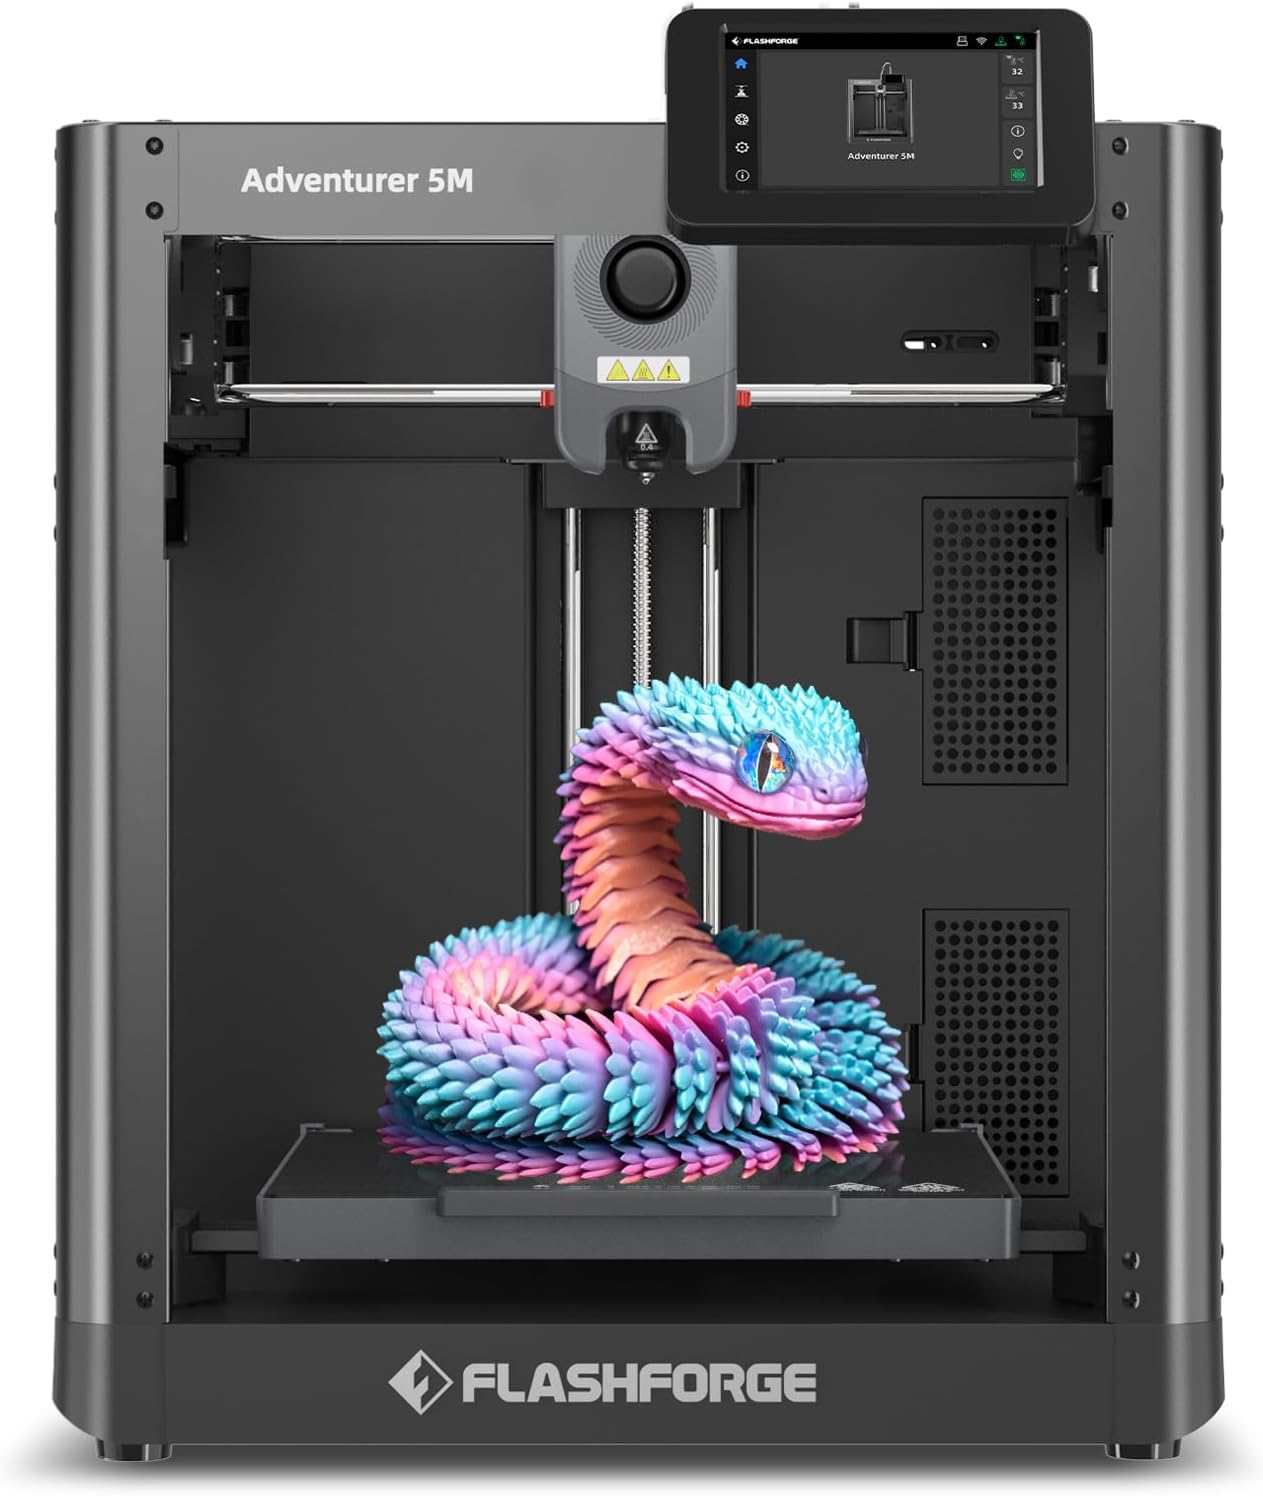
| Build Volume | 220 x 220 x 220 mm |
|---|---|
| Max Nozzle Temp | 280°C |
| Travel Speed | 600 mm/s |
| Platform | Double-sided PEI Platform |
| Structure | All-metal Core XY Structure |
The Flashforge Adventurer 5M is a CoreXY desktop printer focused on speed and convenience for rapid prototyping and small-batch runs. It uses a 280°C direct-drive extruder, quick 3-second detachable nozzles, and a double-sided PEI platform to support a wide range of thermoplastics while making part removal easier. One-button automatic bed leveling and vibration compensation reduce setup time and improve first-layer consistency, and a mobile app offers remote monitoring. The AD5M pushes travel speeds up to 600 mm/s with high acceleration to cut print cycles, and its high-flow nozzle option and multiple nozzle sizes let you trade finer detail for throughput when needed. Practical limits include the modest 220 mm cubic build volume for larger nylon parts and the need to manage moisture-sensitive filaments like nylon with dry storage and tuned settings; printing engineering-grade nylons may require enclosure upgrades and higher nozzle temperatures than standard PLA jobs. For users who prioritize faster turnaround and an integrated, easy-to-use workflow, the Adventurer 5M delivers a capable balance of speed and material versatility.
Best for: Buyers who want a fast, user-friendly desktop printer for prototyping and small production runs and who value automated leveling and quick nozzle swaps to reduce setup time.
Less Ideal for: Users needing large build volume or out-of-the-box capability for high-temperature, industrial-grade nylon parts without adding an enclosure or extensive tuning.
- High travel speed (up to 600 mm/s) and strong acceleration for faster print cycles
- 280°C direct-drive extruder supports a range of engineering filaments
- One-button automatic bed leveling simplifies setup and improves first-layer success
- Quick-detach 3s nozzle and multiple nozzle sizes for fast swaps and throughput tuning
- Dual-sided PEI platform eases part removal and adhesion management
- 220×220×220 mm build volume limits large nylon parts
- May require enclosure or settings adjustments for high-temperature engineering nylons and moisture-sensitive filaments
Verdict: Choose the Adventurer 5M if you want a fast, easy-to-use CoreXY desktop printer that balances high-speed printing with material flexibility for prototyping and small runs.
Creality K2 Combo 3D Printer

| Build Volume | 260×260×260 mm |
|---|---|
| Max Printing Speed | 600 mm/s |
| Max Nozzle Temperature | ≤300℃ |
| Smart Auto Leveling | Yes |
The Creality K2 Combo is a high-speed desktop FDM printer designed to be ready to print quickly while offering advanced features for steady production. It ships largely preassembled and includes one CFS unit for multicolor capability, letting you run multiple filaments without manual swaps and reducing post-print painting. The machine uses step-servo motors and a next-gen direct-drive extruder to push filament fast and maintain consistent extrusion at speeds Creality rates up to 600 mm/s, while a smart auto-leveling sensor probes only the target print area to speed setup. An AI camera gives live monitoring for print failures and idling. In practical use the K2 is aimed at makers who want large, colorful parts out of the box with quieter operation thanks to balanced fans and a low-noise mode. Important caveats: the multicolor functions rely on Creality's CFS ecosystem, and achieving reliable results with challenging engineering filaments like nylon will still require drying, tuned temperatures, and appropriate bed prep despite the printer's capabilities.
Best for: Buyers who want a largely ready-to-run desktop printer that can print multicolor parts and who value quiet operation, automated bed leveling, and built-in monitoring to reduce setup risk.
Less Ideal for: Those who need a printer optimized specifically for high-temp industrial materials out of the box or who prefer an open filament approach without relying on a vendor filament system.
- Large 260×260×260 mm build volume covers most desktop projects
- Preassembled 'plug and play' setup reduces first-print friction
- Supports multicolor printing via CFS modules to avoid manual filament swaps
- Step-servo motors and direct-drive extruder improve extrusion consistency at higher speeds
- Smart auto-leveling and AI camera simplify bed leveling and print monitoring
- Multicolor printing depends on Creality CFS modules and ecosystem
- High-speed printing and multi-material work still require filament drying and tuning for nylon
Verdict: If you want a mostly preassembled, quiet desktop printer that handles multicolor builds and simplifies leveling and monitoring, the K2 Combo is a practical choice.
Choosing the Right 3D Printer for Nylon: Key Factors to Consider
Extrusion Temperature and Hotend Compatibility
Nylon typically prints at higher temperatures than PLA or PETG, so a hotend capable of sustained high-temperature extrusion is essential. Look for all-metal hotends or hotend assemblies rated for at least 260 to 280 degrees Celsius, and confirm the nozzle materials supported. Hardened steel or plated nozzles are beneficial when printing abrasive blends. A hotend that allows easy swapping of nozzles and includes good thermal isolation between the heater block and filament path reduces jams and improves flow stability. Reliable temperature control and a responsive heater circuit help maintain steady extrusion over long prints.
Enclosure and Ambient Thermal Control
Nylon benefits from a warm, stable build environment to reduce warping and layer separation. Enclosures trap heat and smooth ambient swings, which is especially important for large parts. Evaluate whether the printer has a built-in enclosed chamber or can be fitted with an aftermarket enclosure without obstructing motion or electronics cooling. Consider how the machine manages internal temperatures and whether critical components such as stepper motors and electronics are isolated or cooled appropriately. Proper ventilation that does not create drafts across the print is also important for consistent results.
Filament Drying and Handling
Nylon is hygroscopic and will absorb moisture from the air, leading to bubbling, poor surface finish, and reduced mechanical properties. Effective filament handling reduces print failures. Look for printers with spool covers, integrated drying boxes, or straightforward compatibility with external filament dryers. A filament path with minimal exposed travel and a well-supported filament feed helps prevent the filament from tanging or wobbling during long prints. Designs that allow preheating or in-situ drying are useful for a smoother workflow when printing nylon frequently.
Build Surface and Adhesion Strategies
Nylon often has weak adhesion to typical print beds, so a robust bed system is necessary. Heated beds that reach higher temperatures, specialized surfaces like Garolite or textured composite sheets, and the ability to apply adhesives or tapes are all relevant. Consider the ease of cleaning and removing parts once cooled. A removable or flexible build plate can simplify part removal for strong nylon prints. Also assess whether the printer supports a variety of bed materials and whether the bed leveling system can maintain consistent first-layer height across large surfaces.
Mechanical Rigidity and Motion Precision
Dimensional accuracy and mechanical strength of printed nylon parts depend on the printer's frame stiffness and motion quality. Rigid frames and well-supported linear motion systems reduce vibration and layer misalignment that can compromise part performance. Look for quality lead screws or linear guides, and check whether the machine includes features to fine-tune stepper drivers and microstepping. A stable Z-axis and minimal gantry flex are particularly important for tall or high-aspect-ratio nylon parts that undergo sustained extrusion forces.
User Serviceability and Upgradeability
Working with engineering filaments often involves tuning and replacement of consumable parts. Machines that provide easy access to the hotend, clear wiring paths, and user-upgradable firmware make long-term maintenance simpler. Consider whether common upgrades—such as all-metal hotends, direct-drive extruders, or stronger bed mounts—can be added without extensive disassembly. Good documentation and community support reduce time spent troubleshooting moisture issues, hotend jams, or adhesion failures.
Why Nylon Prints Fail and How to Avoid It
Nylon failures usually stem from two root causes: moisture in the filament and uncontrolled temperature differentials during printing. Moist filament can cause steam bubbles and weak layer bonds, while rapid cooling leads to warping and delamination. Address both issues to improve success rates.
Start by storing filament in desiccant-sealed containers or using an inline dryer. Use an enclosure or maintain a warm build chamber to reduce cooling stresses. Adjust print speeds and extrusion multiplier to ensure proper interlayer fusion without over-extrusion artifacts.
- Pre-dry filament at recommended settings before printing
- Use an enclosure or heated chamber for large nylon parts
- Increase nozzle temperature incrementally to improve layer bonding
- Tune first-layer height and print slower for reliable adhesion
Adhesion Techniques for Strong Nylon Parts
Nylon rarely sticks well to bare glass or typical PEI beds without a specialized interface. Mechanical adhesion and chemical aids are common solutions. Choosing the right combination reduces lifts and ensures dimensional stability, especially for functional parts.
Common approaches include textured or composite build surfaces, adhesives applied selectively, and mechanical fixtures like brims or sacrificial rafts for large footprints. Test small samples to find the least invasive method that holds the part during the full print cycle.
- Use textured surfaces such as Garolite or specialized nylon-friendly sheets
- Apply adhesives sparingly at the perimeter rather than across the entire bed
- Add brims or skirts to increase contact area for tall or narrow parts
Filament Storage and Preparation Workflow
A reliable workflow reduces print failures and material waste. For nylon, that workflow starts with moisture control at the spool level and continues through printing. Implement simple, repeatable steps to keep filament dry and ready.
Use sealed tubs with desiccant for long-term storage and a filament dryer or oven for pre-print drying. Label spools with the last dry date and target drying parameters to avoid guesswork. Consider a short hot-end purge routine to clear moisture and contaminants before starting the actual part.
- Store spools in airtight containers with fresh desiccant
- Dry filament using a controlled-temperature dryer before printing
- Purge a small amount of filament at print start to ensure dry material reaches the nozzle
Tuning Print Settings for Durability
To get strong, functional nylon parts, tune extrusion temperatures, cooling, and print speeds rather than relying on defaults. Higher nozzle temperatures generally improve layer bonding, while reduced or no part cooling prevents thermal shocks that cause delamination.
Increase wall count and infill density for structural parts and use slower print speeds for the first few layers to secure the part. Adjust retraction to minimize stringing while preventing clogs, and verify that extrusion multiplier provides full, gap-free perimeters without over-extruding.
- Raise nozzle temperature in 5 degree increments to find optimal layer adhesion
- Disable or minimize part cooling fans when printing nylon
- Use conservative retraction settings to reduce internal stresses and jams
Maintenance Tips to Keep Nylon Printing Reliable
Routine maintenance lengthens the life of core components and keeps prints consistent. Keep the filament path clean and replace wear-prone items like PTFE liners or cracked nozzles before they cause print defects.
Regularly check bed flatness, clean build surfaces, and inspect filter and desiccant status if integrated into the machine. Lubricate linear rails or lead screws per manufacturer guidance and ensure belt tensions remain within recommended ranges to avoid dimensional drift over long prints.
- Inspect and replace worn PTFE tubing or liners
- Check and re-tension belts periodically
- Monitor desiccant and dryer function when in regular use
How We Chose the Best 3D Printer for Nylon
We focused on practical, engineering-driven criteria that matter when printing with nylon and other hygroscopic, high-temperature materials. We evaluated machines for consistent high-temperature extrusion capability, including hotend temperature range and nozzle compatibility, because reliable melting and flow control are essential for strong layer bonding. Thermal management was another key filter: enclosed chambers or effective ambient control reduces warping and improves interlayer adhesion for nylon. Filament handling and moisture control were judged next, emphasizing built-in spool enclosures, active drying, or easy integration with external dryers to prevent brittleness and print failure. Mechanical stability and motion precision were assessed since dimensional accuracy and layer registration affect mechanical part fit and strength. Bed adhesion systems and heated build surfaces were included because nylon often requires specialized adhesives, textured beds, or higher bed temperatures to stick during long prints. We also considered user serviceability and upgrade paths—accessible hotends, nozzle variety, and firmware flexibility—because hobbyists and small shops often tune machines to optimize nylon performance. Excluded from the shortlist were machines lacking sufficient extrusion temperature, open-frame designs without reasonable thermal control, or platforms with poor filament moisture management.
Our full evaluation process is outlined in our review methodology.
FAQ
Do I need an enclosure to print nylon successfully?
Often yes. An enclosure reduces temperature swings and helps prevent warping and delamination, especially for larger parts. Small nylon samples can print on open machines with good ambient control, but an enclosure improves reliability for functional prints.
How should I dry nylon filament before printing?
Use a dedicated filament dryer or a convection oven set to the filament manufacturer's recommended temperature and time. Shorter, lower-temperature drying may not remove deep moisture. Label spools with drying dates to keep track of filament condition.
What bed surface works best for nylon adhesion?
Textured surfaces like Garolite or specialized composite build plates often provide better adhesion for nylon than bare glass or PEI. Adhesives applied selectively and the use of brims can also help secure parts during printing.
Can I print nylon with a Bowden extruder?
You can, but direct-drive setups usually offer more reliable extrusion control for flexible or hygroscopic filaments. Bowden systems can work if the filament path is minimized and retraction settings are carefully tuned, but long runs increase the risk of compression and inconsistent feed.
What nozzle material should I use for nylon blends?
Hardened or plated nozzles are a good choice when printing abrasive nylon blends. Brass nozzles can work for pure nylons but wear faster with filled or abrasive formulations. Choose a nozzle that balances thermal conductivity and wear resistance for your filament type.
Final Verdict
When choosing a 3D printer for nylon, prioritize reliable high-temperature extrusion, a warm and stable build environment, and a filament-handling workflow that prevents moisture absorption. Expect tradeoffs between ease of use and the level of environmental control required for consistent engineering-grade parts. Focus on machines that make it straightforward to dry and deliver filament, maintain steady chamber temperatures, and allow nozzle and bed upgrades so you can tune performance over time.